Notes for owners · Industry playbooks
What an OEM buyer checks before approving a new rubber part supplier
What an OEM buyer checks before approving a rubber part supplier, from compound control to cure records, and why a perfect first sample proves less than evidence that the second batch will match it.
The GullySales team · Updated 17 Oct 2026 · 5 min read
On this page
- Why one good sample proves little in rubber
- Who decides, and what each of them asks
- What the buyer checks, and what to have ready
- Make the approval lot the way production will run
- A moulder near Kottayam and a compressor maker
- When the buyer asks for more than you run
- Write down how the next sample was made
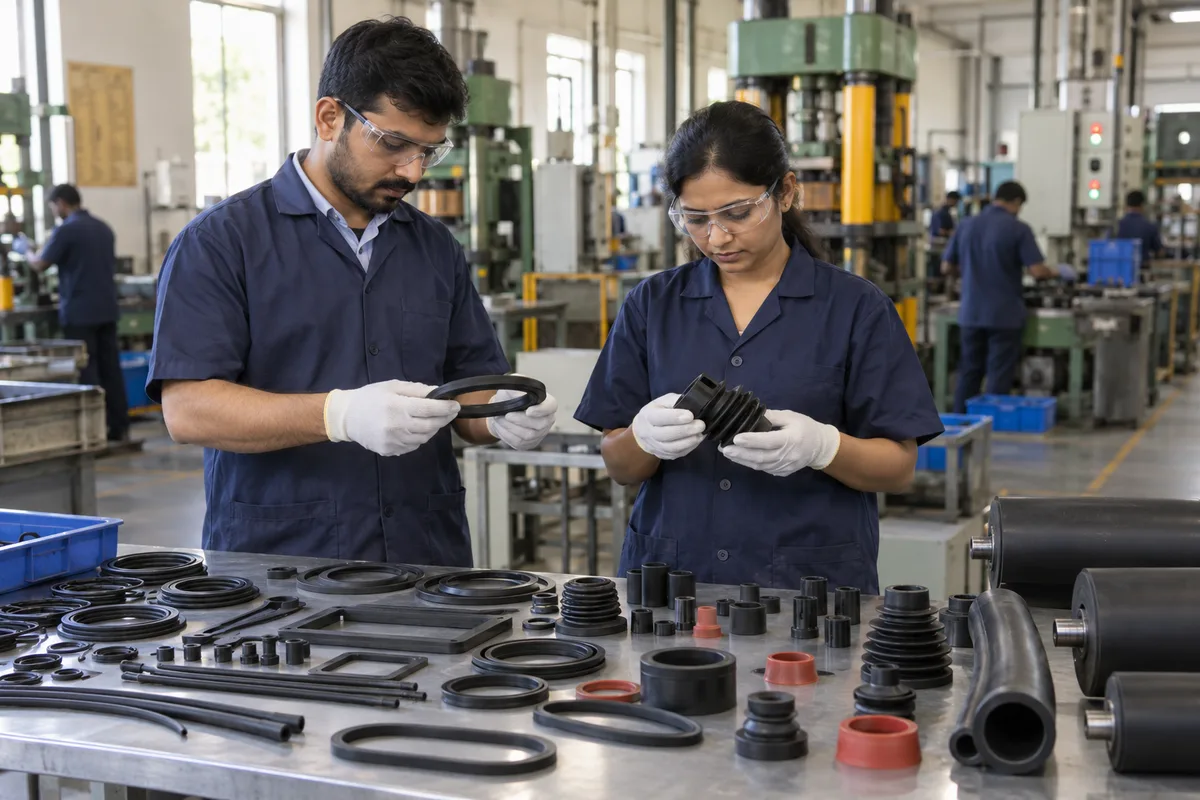
Your sample passed every check: hardness, dimensions, a fit trial on the buyer's assembly. Then the supplier quality engineer asks to visit and wants to see your mixing mill and your batch register before looking at a single part. An OEM buyer approving a new rubber part supplier is judging whether the second batch will match the first. One good sample proves you can make the part once. Approval comes from evidence that your compound, cure and trimming are controlled on an ordinary day, and that a bad lot can be traced to its batch.
Why one good sample proves little in rubber
Rubber is a recipe, not a material off the shelf. The polymer lot, the carbon black, the oil and the curatives all vary. So do mill time, the heat of the day, how long the compound sat before moulding, and the cure time and temperature. Silicone adds post-cure. Flash trimming depends on whose hands do it.
A sample from a small batch, mixed carefully by the owner's best hand, can differ from a production batch mixed on a busy shift. Buyers who have been burnt know this. A careful supplier quality engineer asks how the sample was made before measuring it.
Who decides, and what each of them asks
Three people at the OEM read your approval differently. The development engineer asks whether the part works in the assembly: it seals, fits and keeps its shape after ageing. Purchase asks about price, capacity and whether you can be a dependable second source. The supplier quality engineer asks whether the next ten thousand parts will match these. That signature releases production.
Getting onto the RFQ list in the first place is covered in our post on how industrial buyers decide which unit gets the RFQ. This post starts after your sample has landed on the quality engineer's desk.
What the buyer checks, and what to have ready
These are the checks that come up on a supplier visit for moulded rubber parts, in roughly the order a quality engineer walks the plant.
| What the buyer checks | What it tells the buyer about batch two | What to have ready |
|---|---|---|
| Where the compound comes from | Whether you control the recipe | A recipe code per compound; if bought in, the compounder's certificate for every batch and your own check on arrival |
| Tests on each compound batch | Whether drift is caught before moulding | A batch register with hardness, specific gravity and a cure curve for each batch |
| Raw material storage | Whether old or mixed lots creep in | Labelled lots, first in first out, a use-by date on mixed compound |
| Cure settings | Whether every part is cured alike | A process sheet per part and mould with temperature, time and pressure; press temperature records |
| Mould and cavity marks | Whether a bad cavity can be found | Cavity numbers on parts or bags, a mould maintenance log |
| Trimming and finishing | Whether size varies by operator | The trim method, the gauge or fixture used, the inspection points |
| Lot labels | Whether a complaint can be traced | A bag label with part, compound batch, mould, date and shift |
| Instruments | Whether your numbers mean anything | Calibration status of the hardness tester, rheometer and gauges |
| Change control | Whether you will warn the buyer before changing anything | A written undertaking and the form you use to notify a change |
What happens to that last row once production starts is covered in our post on winning the repeat order for rubber parts.
Make the approval lot the way production will run
The rule is short. Make approval samples from a normal production batch, on the production press, by the operators who will run the job.
Better still, offer parts from two batches mixed on different days, each with its batch test results. If the first sample had to be made by hand from a lab batch, say so on the covering note, and give the date the production-route sample will follow. A quality engineer can forgive a limitation you state. One found unannounced is harder to forgive.
Skip all this for some buyers. A maintenance head replacing one seal on a stopped machine judges you on fit and speed, and a batch register means little that day.
A moulder near Kottayam and a compressor maker
This is an invented example. A rubber moulder near Kottayam makes anti-vibration mounts, and a compressor maker in Coimbatore wants a second source. The owner mixes a small batch of compound by hand and moulds twenty mounts. Every one passes hardness and the buyer's load and deflection test. The supplier quality engineer approves the sample and places a pilot order.
The mill is busy that week, so the pilot lot is moulded from compound bought from a compounder nearby. Hardness sits inside the drawing's band, but at the top of it, and the mounts are stiffer. The compressor vibrates more on the buyer's test bed. The lot is rejected and the approval put on hold.
The owner decides production will use in-house compound only and writes that into the process sheet. Three production batches are mixed on different days, each tested for hardness, specific gravity and cure curve, and moulded into mounts bagged and labelled by batch. The quality engineer is invited to watch a batch being mixed and tested. Approval comes through for in-house compound only, with a line that any change of compound source must be notified first. It costs the moulder a delayed pilot order, three weeks, and a set of test fees.
When the buyer asks for more than you run
Some OEMs, in automotive and appliances among others, work to formal approval schemes with process flow charts, control plans and measurement studies. Their document lists differ by customer and change. Get the list in writing and ask their quality team before assuming anything; our post on the vendor registration pack covers reading one.
A small moulder may not own a rheometer. Say what you do instead, such as bought-in compound with a certificate for each batch plus your own hardness and specific gravity checks. Say too whether you would invest once volumes justify it. Never claim a check you do not run. One invented record can make a quality engineer doubt the rest.
Write down how the next sample was made
Before the next approval sample leaves, note which batch it came from, which press and which operator, and whether production will run the same way. Send that note with the parts. Showing this evidence well is the work of a capability presentation, and the rubber products page is the sector home for these buyers. For the wider selling job, see the sales hub. To set this up for your next OEM, tell us what you need.
Related services