Metal casting foundries · Search engine optimisation
Rank for the alloy and the part, because a buyer searches for a casting, not a foundry.
SEO for a metal casting foundry is the work of appearing when a purchase engineer searches for an alloy, a part or a process, such as SG iron valve bodies or resin sand castings. GullySales builds the alloy pages, the testing page and the technical detail that let search engines and buyers see what you cast.
Scope, fee, reporting and term are agreed in writing after we have read your brief and spoken to you.
What search engine optimisation means
Search engine optimisation (SEO) is the work of getting your website to appear when a buyer searches Google for what you sell. GullySales builds pages around real search terms, fixes technical issues that block ranking, and tracks which searches actually bring enquiries.
Last updated 14 Nov 2026.
For metal casting foundries
Where it usually goes wrong, and what we would do.
“Buyers type the part and the metal”
A design engineer searches for grey iron castings for machine beds or stainless steel pump casings. A site that says only iron and steel castings matches none of those phrases, so the page that should answer the search does not exist.
“Weight and section limits decide the click”
A buyer with a heavy casting scans for the maximum weight you pour. A page without it sends the buyer back to the results to try the next foundry. The limit, stated plainly, is both a ranking aid and a filter that saves you unsuitable calls.
“Photographs of molten metal rank nothing”
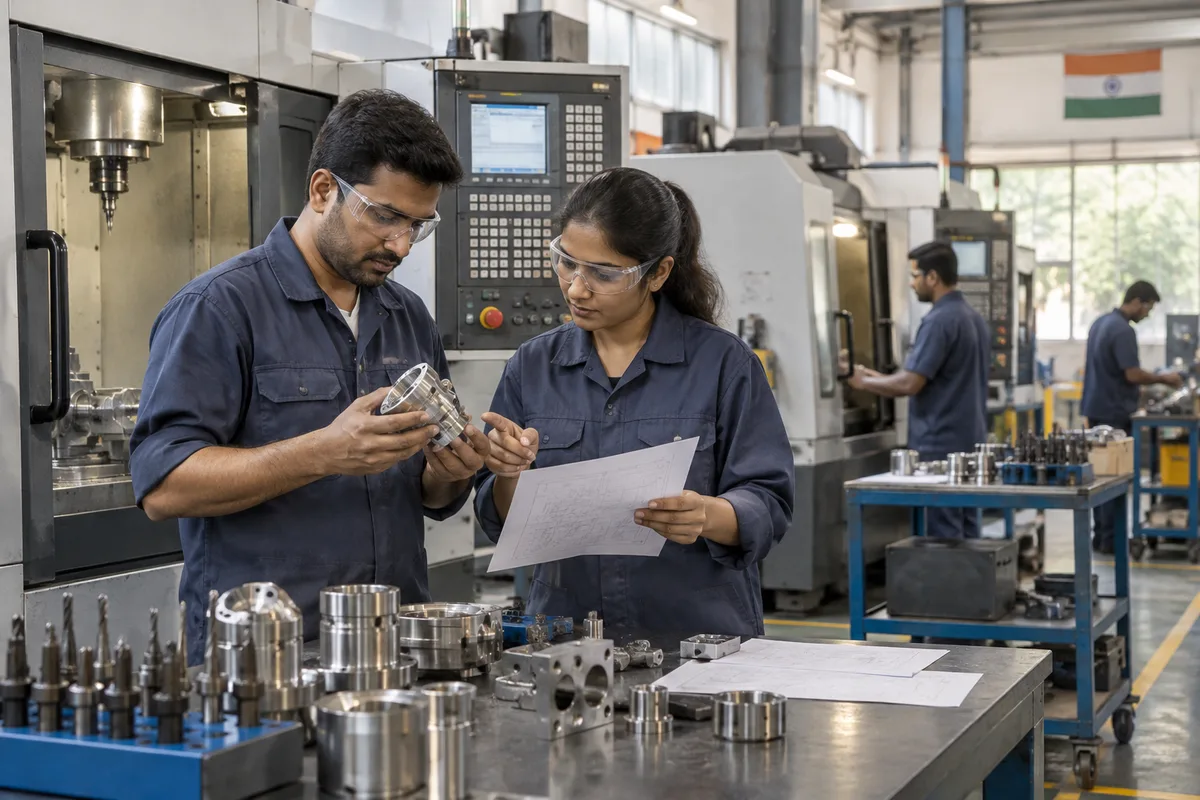
Fire and ladle images carry no words a search engine can read, and a buyer learns nothing from them. A machined casting beside its drawing, with a caption naming alloy and process, gives both the engine and the engineer something to work with.
“Cities in the name are not the whole picture”
Foundry clusters such as Coimbatore, Rajkot and Kolhapur draw searches by place, yet national buyers also search without one. Pages need to serve both: a regional page for nearby plants and alloy pages for the buyer who does not care where you are.
What we do
What we deliver for metal casting foundries.
The work available for this need. We agree the deliverables and responsibilities for your engagement in writing.
Alloy and casting family pages
Separate pages for grey iron, SG iron, steel, stainless and non-ferrous work, each with weight range, moulding method and suitable parts.
Result: Each alloy you sell has a page that can be found by its own name.
A testing and quality page
The spectrometer analysis, mechanical tests, inspection methods and reports issued, with a blanked sample report.
Result: A buyer searching for tested castings lands on a page that shows the tests.
Machined casting pages
Pages for castings supplied finished, with before and after photographs and the machining allowance stated.
Result: Machine builders find a page for the finished part.
Image captions and file names
Photographs of patterns, moulds and finished parts named and captioned with alloy and part.
Result: Your image folder reads as a list of what you cast.
A technical fix list for the site
Speed, mobile layout, page titles, headings and links checked, with the fixes listed in the order they matter.
Result: You hold a written list of what was found and what was changed.
Search tracking by page
Search impressions, clicks and enquiries read page by page against a baseline noted at the start.
Result: You can say which alloy page brings drawings.
How the result is measured
- Ranking positions
- Organic traffic
- Enquiries from organic search
Recorded as a baseline before work starts, so every later report has an honest comparison.
Searches your buyers type
Pages for the alloys and parts a buyer searches by name.
- grey iron castings manufacturer
- A page for grey iron with the weight range, moulding method, grades poured and the parts you cast, such as machine beds and housings.
- SG iron casting supplier for valves
- A page for ductile iron naming the grades, the test reports issued and the valve and fitting parts you have poured.
- steel castings for heavy engineering
- A steel page with maximum weight, heat treatment you offer and the sectors you supply, written for a design engineer.
- stainless steel pump casings
- A page for stainless work with grade names, the pour method and the inspection supplied with each lot.
- casting foundry with pattern making
- A page on your pattern shop, the materials used, who owns the pattern and how storage and repair are handled.
Who it is for
This is written for these metal casting foundries.
- Grey iron foundries for machine tools, pump casings and brake parts
- SG iron and ductile iron foundries for valves, pipe fittings and auto parts
- Steel casting foundries for heavy engineering and railways
- Non-ferrous foundries for brass, bronze and aluminium gravity castings
- Stainless steel foundries for pumps and process equipment
- Shell moulding and resin sand foundries making precision castings
- Foundries with in-house pattern shop and machining
- Small jobbing foundries serving local engineering units
Before you decide
When this may not be the right fit.
- You cannot state your weight range or grades without checking with the plant head, so the pages would be vague.
- Your foundry takes only work from existing customers and has no capacity for a new alloy, so a page would draw enquiries it cannot serve.
Before you decide
Agree the work. Know how to judge it.
SEO for foundries: use these checks to prepare, choose the scope, and review what changes.
Bring the right evidence
Bring the pages for the products or services you want to sell, the search queries available in your reports, and examples of enquiries from search. Separate branded searches from buyers discovering you for the first time.
Make the scope clear
Agree which pages and technical fixes come first, who can publish changes, and who supplies subject knowledge. Link search work to a relevant enquiry route on each priority page.
Check the work in use
Follow the trail from a relevant query to its landing page and then to an enquiry. Review whether those enquiries fit your offer, alongside indexing and search visibility.
Know when to change course
A ranking movement alone is not a buying signal. If traffic grows but relevant enquiries do not, revisit page intent and the offer before producing more pages.
These are discussion points, not a fixed package. GullySales confirms the deliverables, responsibilities, fee, and term in writing after reading your brief and speaking with you.
Before we start
What to have ready before the work starts.
The records, access and decisions this work needs from metal casting foundries. Anything missing is noted in the written scope, with who will supply it.
- Weight and section limits for each alloy
- The smallest and largest weight per piece and the section thickness range the foundry can pour in each metal. A page without these limits is skipped by the buyer who is checking whether the part fits. If the limits are not written down, a senior moulder or the owner states them and we record them.
- The grades and specifications actually poured
- A list of the grades and standards the foundry pours to, by name. Do not list a grade the foundry has never poured. If a grade is poured only on request, say so. Without this list, we state the metals only in general terms and lose the buyer who searches by grade.
- Search console and analytics access
- Access to the site's search data lets us record what the foundry appears for before changes. If neither tool is installed, tell us who holds the domain. Without a starting record, the later comparison cannot show what the new pages changed.
- Photographs of finished and machined castings
- Sharp photographs of finished castings, machined parts and the pattern shop, cleared by the customer where a part is recognisable. Phone pictures in daylight are acceptable. Where none are cleared, the pages use shop-floor and process pictures, which answer the first doubt but show less of the finished work.
How it works
How the search engine optimisation work runs
The work itself, in order. How an engagement starts, from your brief to a written scope, is set out on our method page.
- 1
List the alloys and casting families poured
We start from the foundry's own order book and pattern list, and note each metal and casting family it actually pours: grey iron, SG iron, steel, stainless or non-ferrous, and the parts made from each. You mark the ones with the best margin. This becomes the set of pages the site needs, since buyers type the part and the metal.
- 2
Search as a purchase executive would
We search for the parts and metals a buyer types, such as SG iron valve bodies or grey iron machine beds, and record which foundries and which kinds of page appear. You tell us which of them you meet in real quotations. This shows the words buyers use and the limits they check first, such as weight and section.
- 3
Record present visits, searches and enquiries
Before any page is changed, we note the searches the site appears for, the visits it gets and the enquiries it produced, using the search console and analytics if they exist or setting them up first. These are the figures the last step is read against, so nothing is edited until they are written down.
- 4
Write each alloy page with a metallurgist
We sit with the foundry's metallurgist or quality head to write a page for each alloy and casting family: the grades, the weight range, the moulding method, typical parts and the tests that go with them. The metallurgist corrects every figure against the shop's records. A page without limits answers no buyer's question.
- 5
Build the testing page from real reports
We write a testing and quality page that describes the analysis, mechanical tests and other checks the foundry does, using the reports you give us with customer names removed. Machined castings get a page of their own. Photographs carry plain captions and file names, since a picture of molten metal ranks for nothing, and the figures are read against the starting record.
Where this fits
Three pieces of sales work, in this order.
This work sits inside sales process design, at stage 1, prospecting and lead generation. The audit comes before it, and sales management keeps it running.
Step 1
Sales audit
Find where deals are being lost and what to fix first.
Start here if you cannot say where orders are lost.
Step 2 · you are here
Sales process design
One written way to sell, from first enquiry to repeat order.
Start here if every salesperson sells differently.
Step 3
Sales management
A target, a review routine and someone who owns the number.
Start here if the team has targets and no routine.
FAQ
Questions owners ask before they call.
Not here? More answers, or ask on WhatsApp.
How do we know SEO is working for a foundry?
Do we need a page for every part we have cast?
Do we need a page for every part we have cast?
How do we know SEO is working for a foundry?
Should the page list our customers by name?
Do we need a separate page for every pattern we hold?
How much does it cost?
How long is the contract?
How soon will we see results?
Who will actually do the work?
More for metal casting foundries
Related work to consider.
Closest to this: search and visibility
Also for metal casting foundries
Or start from the overview: sales and marketing for metal casting foundries.
Your next practical step
Tell us what you are trying to grow, and we will read it before we call.
Eight short steps, mostly taps. Skip anything you would rather answer on the call.