Manufacturing · Forging & Metal Forming
The progressive die made us efficient, and it also made us dependent on one part number.
Stamping is a numbers game. A progressive die costs a great deal, then makes parts for years at a low cost per piece. The stamper wins by running the same die for the same buyer, and loses when that buyer's volume drops or a model ends.
Scope, fee, reporting and term are agreed in writing after we have read your brief and spoken to you.
In one paragraph
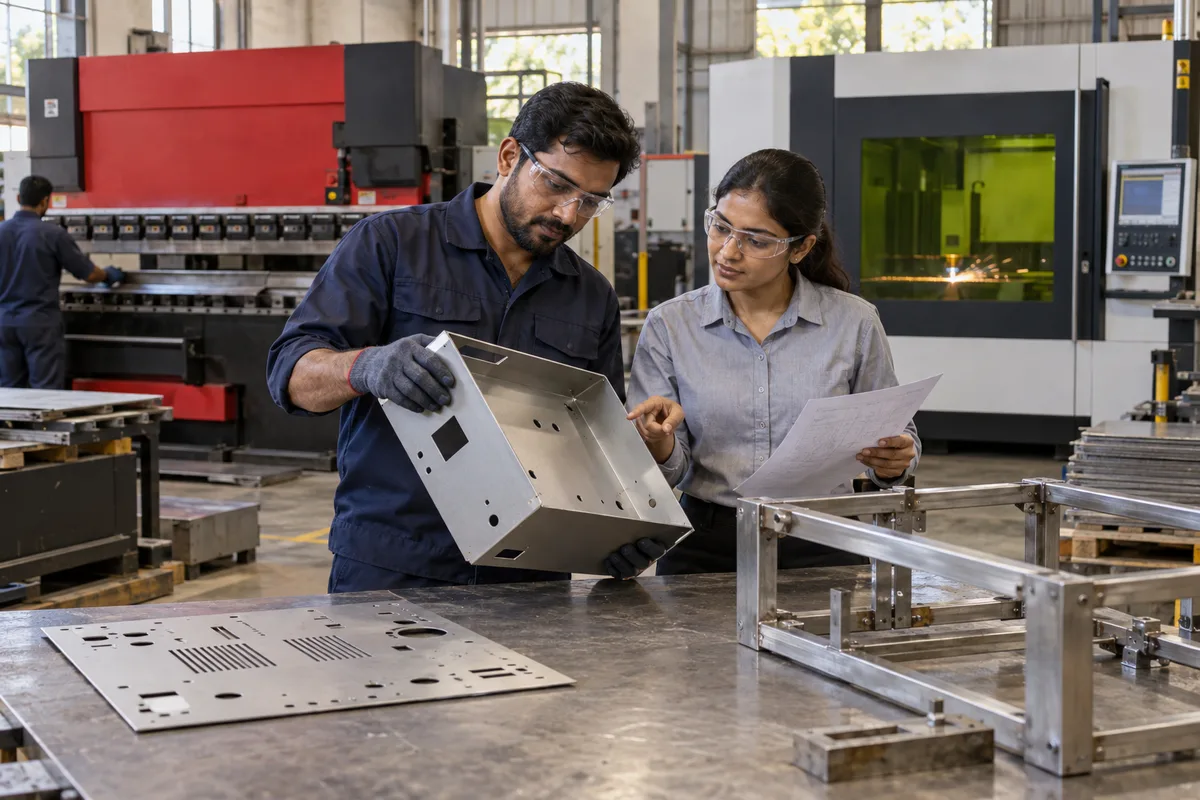
Metal stamping presses sheet or strip metal between dies to blank, pierce, bend and form parts at speed, in progressive, compound or single-stage dies. GullySales helps stampers show the press tonnage, strip widths and tooling they run, so buyers of brackets, terminals, clips and housings can judge fit before sending a drawing.
So the work is to find the next die: the next bracket, terminal or clip for a buyer who is not yet on the books. That means reaching purchase engineers at electrical, appliance, automotive and furniture firms before they have chosen.
Last updated 16 Oct 2026.
Who it is for
This is written for you if metal stamping is what you make or sell.
- Press shops running progressive, compound and single-stage dies
- Stampers with in-house tool room and die maintenance
- Units making terminals, brackets, clips, washers and housings
- Shops that also plate, weld or assemble the stamped part
Not for
It is not the right fit if.
- A shop without a tool room or a die maker it trusts, since every new part begins with a die
- A unit that wants to bid on very low volumes where a die cannot be justified
How buyers choose
What decides the sale of metal stamping.
Strip width, thickness and press tonnage
The engineer checks whether your presses and feeders suit the material and part size. A clear table of press tonnage and strip range saves a call.
Die cost and ownership
A progressive die is a separate cost with its own approval. Buyers want a die quotation with ownership, expected life and maintenance terms stated.
Material and its finish
Steel, stainless, copper, brass or aluminium strip is named on the drawing, with plating or coating where needed. Buyers ask who supplies and who finishes.
First-article approval and control plan
A sample from the die is measured and a plan agreed for inspection in production.
Where orders are lost
What usually goes wrong when you sell metal stamping.
In the words owners use on the first call.
“Our dies are running the same parts for the same buyers”
Nobody is building the pipeline for the next die. When one buyer slows down, the press hours go empty.
“The die quotation was too high and the buyer went quiet”
The shop never explained the die cost against life and piece price. The buyer could not take the number to their committee.
“Buyers search for the part and we sell the process”
A search for a terminal or a clip does not find a page about stamping presses.
The scope
The work we would propose for metal stamping.
Measured on qualified enquiries, quotation requests, follow-up on each quotation, trial orders won and repeat orders. Anything here that needs a platform, directory or tool we have not used with you is confirmed with you before it goes in the scope.
- Part-family pagesPages for terminals, brackets, clips and housings, each saying what dies and materials you run.
- A die-quotation format that explains the dieDie cost, life, ownership and piece price set out clearly, with a follow-up call to the buyer's committee contact.
- Prospecting among electrical, appliance and furniture makersNamed firms who buy stamped parts and the part types they use.
- Marketplace listings by partEntries by part and material, with a reply that asks for the drawing and annual quantity.
A tooling register
A sheet of each die, who owns it, when it last ran and the next call to the buyer.
What we do
What you get for metal stamping.
Each deliverable and what it is there to change.
A press and strip range sheet
Tonnage, bed size, feeders and material range in one page.
A die-quotation template
Makes the die cost understandable to a purchase committee.
A tooling register
Dies, owners, last run and next call.
A part-family buyer list
Named buyers of terminals, brackets and clips.
How the result is measured
- Die quotations requested
- Die quotations followed up
- New dies approved
- Sample approvals
- Repeat releases on existing dies
- Press hours sold against idle
Recorded as a baseline before work starts, so every later report has an honest comparison.
How it works
From your first message to the first report.
No open-ended retainer. Every step gives you something in writing.
First
Your brief
You tell us what you need in a few short steps: your business, what you want, where enquiries come from and how they are handled.
After the brief
A conversation and a written scope
We read it, then talk with whoever handles your enquiries. If you want our help, the scope, the fee and the reporting come in writing, and nothing starts before you have read them.
Before work starts
Baseline recorded
The numbers this work is meant to move, such as enquiries, quotations, orders, visits or renewals, written down so every later report has an honest comparison.
After the baseline
The first fix goes live
The fix we agreed to start with is put in place and measured against the baseline, whether that is a reply, a follow-up, a page, a listing or the handover between marketing and sales.
As agreed
Report against the baseline
What moved, what did not, and what changes next, in plain words. How often you get it is set in writing before work starts.
At renewal
Renew on the numbers
The term ends and you decide whether to continue from the results. The length is agreed in writing before anything starts.
What we need from you
What to have ready before we talk.
None of it has to be tidy. We read what you have.
- Press list with tonnages and bed sizes
- Dies held and for which customers
- Materials and platings you handle
- Recent die quotations and their outcome
- Photographs of stamped parts
Export and new regions
Selling metal stamping beyond your home market.
Where you sell decides standards, documents, payment terms and freight. We work from Bengaluru and have no overseas office, so for a new region we start from your own enquiries, your existing buyers and the directories you already use.
Overseas OEMs buying stamped parts
Electrical and appliance makers abroad source stamped parts through agents and direct vendor lists. Your own export enquiries show which route reaches you.
Die ownership and shipment
A foreign buyer may want to own and later ship the die. Agree who does what before the die is made.
FAQ
Questions about selling metal stamping.
Not here? More answers, or ask on WhatsApp.
How do stamping buyers find a new supplier?
Should we explain die cost on the website?
How do we keep the press full between die orders?
How long is the contract?
How soon will we see results?
Who will actually do the work?
What do you need from us?
What if we are not happy with the work?
More in Forging & Metal Forming
Makers of metal stamping also need
Looking for the wider industry page? See steel rolling mills and tmt bar makers.
This page is part of the manufacturing section. The hub also lists every manufacturing industry we write for.
Why us
Why owners pick GullySales over an agency.
Marketing and sales, as one job
Most agencies stop at the enquiry. We also fix what happens after it: the reply, the follow-up, the quote and the CRM.
The person on the first call does the work
No account managers in between. You are never handed to someone you have not met.
A baseline before anything starts
Your numbers are written down on day one, so every later report compares against something honest.
The fee in writing, split three ways
Our time, your media spend and production on separate lines. You always see what goes to us.
No guarantees we cannot keep
The term is agreed in writing and never a default twelve months. We never promise a ranking or a lead count, because nobody controls those.
One office, and we say so
Nagarbhavi, Bengaluru. We work across India by call and WhatsApp and travel when a session needs to be in person.
#257, 3rd floor, Sri Nanjundeshwara Complex, Nagarbhavi 8th Block, Outer Ring Road. How we work.
Engagement options
Ways to work with us.
Pick the size of commitment that fits. Every option starts with your brief and a conversation.
Option 1
The conversation on its own
A call after you send your brief. It says honestly whether you need outside help, and many fixes are ones your own team can make.
Option 2
One fix, scoped
Start with the fix that matters most, such as reply time or follow-up. The fee is in writing before anything starts.
Option 3
An ongoing programme
We run the work, report against the baseline, and you renew on the numbers. The term and the reporting are agreed in writing first.
Option 4
Guidance for your own team or agency
We plan, brief and check the work of your in-house team or current agency, instead of replacing them.
Your brief
Tell us what you need, and we will read it before we call.
Eight short steps about your business, what you want and who decides. Most questions are a tap, and you can skip any you would rather answer on the call.
Your next practical step
Tell us what you are trying to grow, and we will read it before we call.
Eight short steps, mostly taps. Skip anything you would rather answer on the call.